A TPE compound may feel rubber-like in service even though production relies on melting, cavity filling, cooling, and controlled release. Their flow and shrinkage respond to material grade, moisture, temperature, pressure, speed, and mold conditions. The practice of injection molding rubber materials such as TPE requires disciplined control from storage through finished-part stabilization.
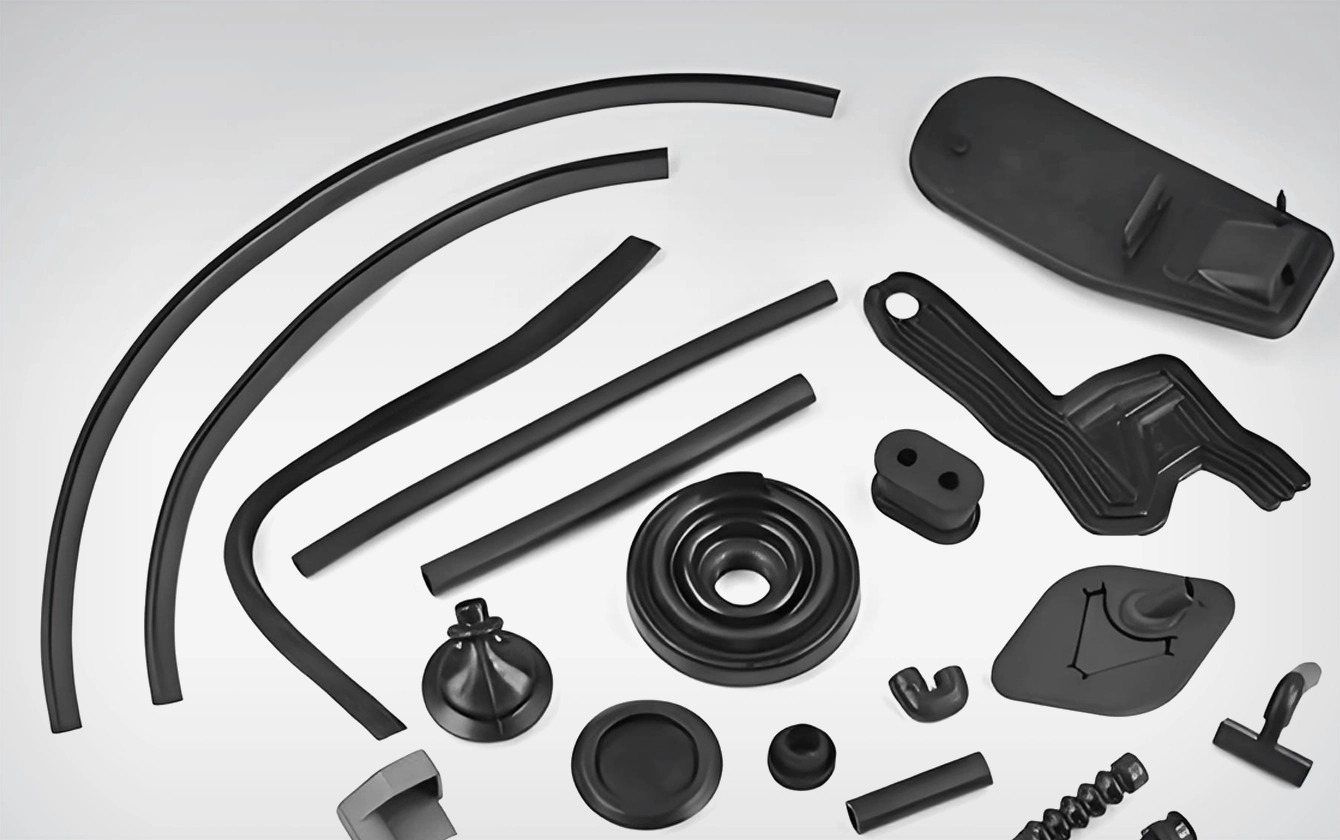
For TPE, repeatability depends on how material preparation and cooling work together. Lot condition, drying requirements where applicable, melt response, cavity balance, mold temperature, cooling-water stability, and the time allowed for dimensional stabilization should be studied as one process window. This focus separates TPE molding from thermoset-rubber discussions that center on vulcanization. Consistent preparation, responsive injection, balanced cavities, uniform cooling, careful ejection, and traceable inspection must operate within one verified process window.
Control Lot Condition and Material Preparation
Material qualification must look beyond hardness because melt response, thermal stability, shrinkage, bonding, and cooling behavior affect the process in different ways. Supplier data establishes initial processing guidance. Trials with the production mold and equipment determine the ranges that produce acceptable dimensions and surfaces.
Dekuma configures its RV-Se platform for TPV, TPE, flexible modified PVC, and other suitable injection-moldable compounds. The machine uses servo hydraulics, pressure feedback, and rapid response for demanding automotive and industrial applications.
Dekuma’s approach to injection molding rubber materials should be validated with the selected TPE grade, mold, cooling arrangement, and handling method. Comparing cavity and cycle data shows whether a change improves filling and stabilization together or merely shifts defects to a later stage.
Material lot, storage temperature, moisture where relevant, colorant, and regrind ratio should be controlled. Automatic feeding repeats the supplied condition. It cannot prevent variation when unapproved or inadequately prepared material enters the system.
Purging and first-off approval are necessary after grade or color changes. Residue may alter appearance, bonding, or properties. Production should resume only after the material path, recipe, and sample results meet the release criteria.
Balance Melt Response and Cavity Filling
In TPE injection molding, high flow may be needed to reach thin or distant details before cooling restricts movement. Excessive speed can trap air or create flash. The fill profile must be matched to gates, vents, and cavity geometry.
The RV-Se compares actual pressure and flow with commands through pressure sensors, encoders, a servo motor, and PID control. Monitoring response, switching position, cushion, and holding pressure helps identify drift before dimensions or weight move outside limits.
Short-shot studies and cavity-level weights show how the mold fills. A combined average can hide one restricted or overheated cavity. Adjustments should rely on location-based evidence rather than a single overall part measurement.
Servo pump output follows real pressure and flow demand. This may reduce unnecessary energy use. Performance should be calculated per accepted part and include barrel heating, mold temperature control, cooling, robots, idle periods, and scrap.
Validate Cooling and Dimensional Stabilization
TPE generally solidifies through cooling, so mold temperature and channel balance influence both cycle time and final geometry. Removing a soft part too early may shift deformation downstream even when cavity filling was stable.
Cooling studies should compare dimensions after the full stabilization period. A shorter setting may appear successful at the press but fail after stacking, conveying, or assembly. Support fixtures and end effectors should avoid concentrating force on warm profiles.
Water flow, filters, channels, sensors, and mold deposits can gradually change heat removal. Temperature mapping and preventive maintenance help separate cooling problems from injection or material causes.
Cycle optimization should use accepted output per available hour. Faster injection provides little benefit if cooling, handling, or inspection remains the constraint. Balanced improvements protect quality while increasing real capacity.
Mold qualification should document temperature distribution, cavity balance, vent condition, and release behavior. The same study should be repeated after major repair so the restored tool can be compared with its approved baseline rather than judged only by appearance.
Holding pressure and time influence shrinkage and sink behavior after filling. Excessive holding may add stress or flash, while insufficient holding can create dimensional variation. Part weight and stabilized dimensions provide practical evidence for the selected profile.
Preventive maintenance should include the screw, check components, heaters, sensors, hydraulic response, cooling circuits, ejectors, and robot tooling. Changes in recovery time, cushion, pressure, or mold temperature can indicate a developing issue before yield falls sharply.
Production interruptions need material-specific restart rules. Melt held for too long may degrade, while an insufficiently stabilized mold can shift dimensions. Purge quantity, temperature recovery, and first-off sampling should be defined in the operating method.
Downstream feedback adds another quality signal. Assembly force, fit, sealing performance, or bonding results may reveal variation that normal visual inspection misses. Linking those results to cavity and process history supports more targeted improvement.
Use Quality Data to Protect the TPE Window
Injection molding rubber materials requires records that connect material grade and lot with melt temperature, pressure profile, speed, holding, cooling, cavity, and inspection. Access control and revision notes protect the approved recipe.
Inspection may include part weight, dimensions, surface condition, flash, short filling, and bonding. The measurement system should be checked with reference parts so changes in gauges, fixtures, cameras, or lighting are not mistaken for product variation.
Stable TPE injection molding results from controlling material condition, fill response, cooling, and handling together. When maintenance and inspection preserve the validated window, production teams may improve yield through targeted evidence instead of repeated adjustments to several variables at once.